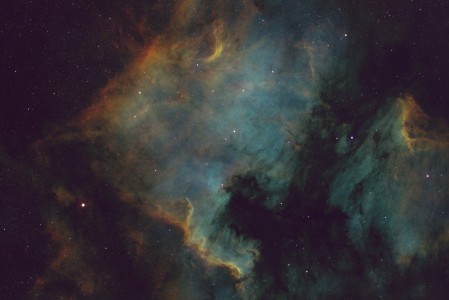
Hi Jon,
Roland's lens correction per AP website:
Optical Production and Testing Standards
Every production run starts with optical glass purchased to our specifications. Each blank is inspected and tested by our suppliers to meet our homogeneity and quality standards. These blanks are then processed in our computerized facility and hand-figured by experienced opticians. Each surface is polished to a fine sphere and tested by test plate interferometry. Three elements are then matched and assembled as a set. Final figuring on the front and rear surfaces is done using our green light Fitzeau interferometer which checks the wavefront accuracy. The interferometer immediately shows when a polishing lap is worn when zones develop on the glass surfaces. A new lap can then be made without guesswork to again produce a smooth surface.
The finished lens is then coated and assembled in a precision cell which is fully temperature-compensated. The cell is attached to the tube assembly and the optical alignment is checked at high power on an artificial star. The lens is serialized and all test data including final interferogram are stored in a computer file along with the customer's name. Our extensive hand-figuring techniques and the use of high quality blanks allows us to guarantee that all production lenses will meet the 1/50 RMS (98.4% Strehl ratio) minimum limit.
Roland's lens correction per AP website:
Optical Production and Testing Standards
Every production run starts with optical glass purchased to our specifications. Each blank is inspected and tested by our suppliers to meet our homogeneity and quality standards. These blanks are then processed in our computerized facility and hand-figured by experienced opticians. Each surface is polished to a fine sphere and tested by test plate interferometry. Three elements are then matched and assembled as a set. Final figuring on the front and rear surfaces is done using our green light Fitzeau interferometer which checks the wavefront accuracy. The interferometer immediately shows when a polishing lap is worn when zones develop on the glass surfaces. A new lap can then be made without guesswork to again produce a smooth surface.
The finished lens is then coated and assembled in a precision cell which is fully temperature-compensated. The cell is attached to the tube assembly and the optical alignment is checked at high power on an artificial star. The lens is serialized and all test data including final interferogram are stored in a computer file along with the customer's name. Our extensive hand-figuring techniques and the use of high quality blanks allows us to guarantee that all production lenses will meet the 1/50 RMS (98.4% Strehl ratio) minimum limit.

