What is the 'best' way to make the focuser hole in a 12" dia. .094 Hastings Aluminum tube?
My last attempt, in a 6" dia. .094, used a round metal hole saw and was messy and needed a lot of filing and cleanup. The center bit drill chewed a bigger hole in the aluminum and the hole saw chattered around a bit. Fortunately, I used one that was smaller than needed so filing cleanup took away most of the damage!
I expect that a 'Greenlee' style threaded hole punch would distort the tube.
I'm putting in a 2" DAR dual Helical Focuser, so the hole will probably need to be over 2 1/2" (I'll get an exact measurement when I take it off the old tube!).
I suspect that there's no easy way, but any helpful hints would be appreciated.
Thanks.
Mike
6" f6 homemade on old Meade GEM
10" f4.5 homemade on old Meade GEM (WSP2008 Version!)
My last attempt, in a 6" dia. .094, used a round metal hole saw and was messy and needed a lot of filing and cleanup. The center bit drill chewed a bigger hole in the aluminum and the hole saw chattered around a bit. Fortunately, I used one that was smaller than needed so filing cleanup took away most of the damage!
I expect that a 'Greenlee' style threaded hole punch would distort the tube.
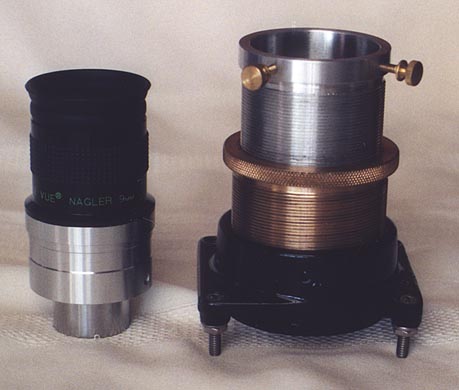
I'm putting in a 2" DAR dual Helical Focuser, so the hole will probably need to be over 2 1/2" (I'll get an exact measurement when I take it off the old tube!).
I suspect that there's no easy way, but any helpful hints would be appreciated.
Thanks.
Mike
6" f6 homemade on old Meade GEM
10" f4.5 homemade on old Meade GEM (WSP2008 Version!)
Attached Image: